OEE Software for Injection Moulding Machines: Improve Production Efficiency and Machine Performance
Injection moulding is a widely used manufacturing process for producing plastic components across industries such as automotive, electronics, consumer goods, packaging, medical devices, and household products. Production facilities often operate multiple injection moulding machines with different moulds, materials, cycle times, and production requirements.
Although these machines are designed for repeatable and high-volume production, maintaining consistent performance can be challenging. Unexpected machine stoppages, longer cycle times, mould changes, material-related issues, and rejected components can reduce actual production output.
For production managers, knowing how many components were manufactured during a shift is not enough. They also need to understand how efficiently each machine operated, how much time was lost, and whether the produced components met quality requirements.
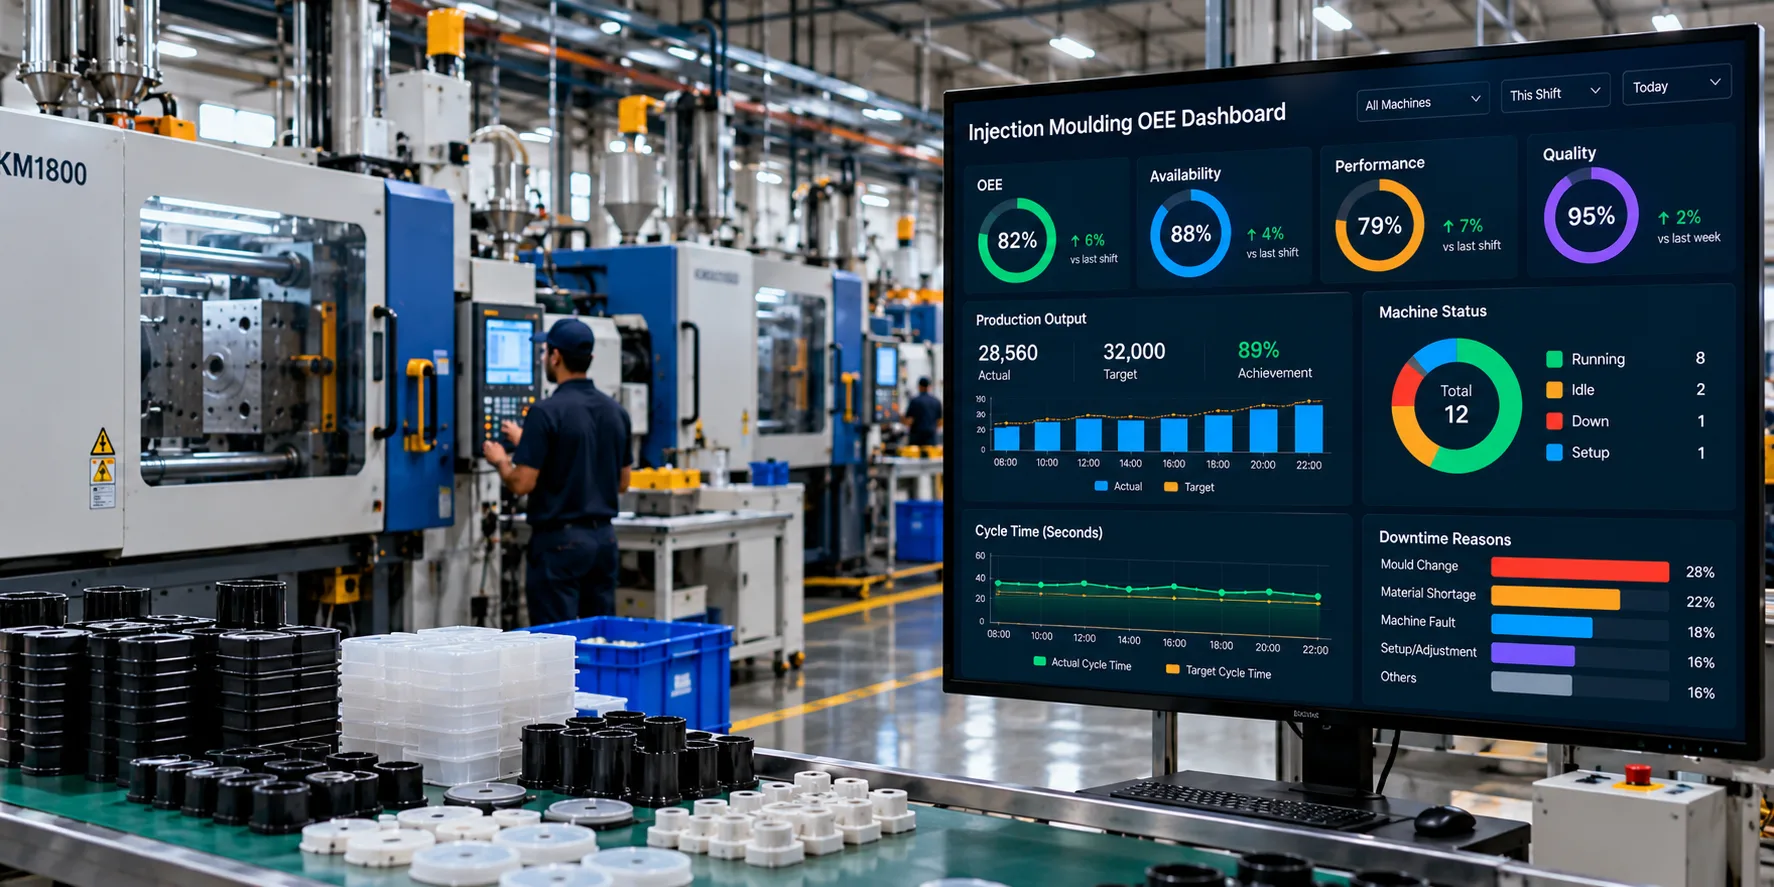
This is where Injection Moulding OEE Software becomes valuable. It helps manufacturers monitor availability, performance, and quality to understand overall equipment effectiveness and identify opportunities for improvement.
With reliable production data and real-time visibility, injection moulding facilities can move beyond manual production records and make better decisions about machine utilisation, downtime, and production planning.
What Is Injection Moulding OEE Software?
Injection Moulding OEE Software is a production monitoring solution that measures the effectiveness of injection moulding machines using three core OEE parameters: availability, performance, and quality.
It helps manufacturers understand how effectively machines convert planned production time into good-quality plastic components.
For an injection moulding facility, the software can help monitor information such as:
Machine running and stopped status
Actual production counts
Expected and actual cycle times
Machine downtime and stoppage reasons
Rejected and good-quality components
Shift-wise production performance
Machine-level OEE
Production targets and achievement
The exact data available depends on the machine controller, connected signals, sensors, and system configuration.
By bringing this information together, production managers can identify where production losses are occurring and take action based on actual operating data.
Why Injection Moulding Manufacturers Need OEE Monitoring
Injection moulding operations have several process-specific factors that influence production efficiency. Even a small interruption or performance variation can affect output when machines are expected to operate continuously.
1. Frequent Machine Downtime
Injection moulding machines may stop because of hydraulic or electrical faults, temperature-related issues, material shortages, mould problems, or maintenance requirements.
When stoppages are recorded manually, the actual duration and reason may not always be captured accurately.
A monitoring system helps record machine interruptions and provides visibility into how much planned production time is being lost.
2. Variation in Cycle Time
Cycle time is one of the most important performance indicators in injection moulding.
Each production job has an expected cycle time based on factors such as material, mould design, component geometry, cooling requirements, and process settings.
However, actual cycle time may increase because of process adjustments, cooling delays, material behaviour, or equipment-related issues.
Monitoring actual cycle time against the approved reference helps production teams identify machines or jobs that are not meeting expected production rates.
3. Mould Changeover and Setup Losses
Manufacturing facilities frequently change moulds to produce different components.
Mould installation, removal, setup, trial runs, parameter adjustments, and quality approvals can consume production time.
Without structured monitoring, these activities may be grouped together as general downtime, making it difficult to understand how much time is spent on changeovers.
Recording setup and changeover activities separately helps managers investigate opportunities to improve production scheduling and reduce avoidable delays.
4. Rejected Components and Quality Losses
Injection moulding quality can be affected by several process variables, including temperature, pressure, cooling time, material condition, and mould performance.
Common defects include:
Short shots
Flash
Sink marks
Warpage
Burn marks
Surface defects
Dimensional variations
Rejected components reduce the number of good parts available for dispatch and can increase material consumption and rework.
Tracking quality alongside production output helps manufacturers understand how quality losses affect overall equipment effectiveness.
5. Limited Production Visibility Across Machines
A factory may operate several injection moulding machines with different capacities, tonnages, mould configurations, and product requirements.
When production information is maintained separately through spreadsheets, paper registers, or operator reports, comparing performance becomes difficult.
A centralised OEE dashboard can provide a consolidated view of machine status, output, downtime, and efficiency across the production floor.
Understanding OEE for Injection Moulding Machines
Overall Equipment Effectiveness measures how effectively a machine operates during its planned production time.
OEE is calculated using three factors:
OEE = Availability × Performance × Quality
Each factor highlights a different category of production loss.
1. Availability
Availability measures the percentage of planned production time during which the machine was actually operating.
Availability = Operating Time ÷ Planned Production Time × 100
For example:
Planned production time: 450 minutes
Machine downtime: 45 minutes
Actual operating time: 405 minutes
Availability:
405 ÷ 450 × 100 = 90%
This means the machine was available for production during 90% of its planned production time.
2. Performance
Performance measures whether the machine is producing at its expected cycle rate.
Performance = Ideal Cycle Time × Total Pieces Produced ÷ Operating Time × 100
Suppose an injection moulding machine has:
Ideal cycle time: 30 seconds
Number of cavities: 2
Operating time: 405 minutes
Actual production: 1,500 components
The ideal output during operating time would be:
405 × 60 ÷ 30 × 2 = 1,620 components
Performance:
1,500 ÷ 1,620 × 100 = 92.59%
This indicates that actual production was below the expected output based on the reference cycle time.
For multi-cavity moulds, the calculation must use a consistent production unit. If output is measured in individual components, the cavity count must be included. If output is measured in completed moulding cycles, the ideal cycle-time calculation should use the same unit.
3. Quality
Quality measures the percentage of total production that meets the required quality standards.
Quality = Good Pieces ÷ Total Pieces Produced × 100
Suppose the machine produces 1,500 components, of which 1,470 pass quality inspection.
Quality:
1,470 ÷ 1,500 × 100 = 98%
The remaining components represent quality losses that may require investigation.
4. Overall OEE Calculation
Using the above example:
Availability: 90%
Performance: 92.59%
Quality: 98%
OEE:
90% × 92.59% × 98% = 81.63% approximately
This gives production managers a combined view of how effectively the injection moulding machine used its planned production time.
The calculation is only meaningful when planned production time, machine cycles, cavity counts, and good-part definitions are consistent.
Key Features of Injection Moulding OEE Software
An effective OEE monitoring solution should provide more than a production counter. It should help manufacturers understand machine behaviour and identify the reasons behind production losses.
1. Real-Time Machine Status Monitoring
Machine status monitoring provides visibility into whether an injection moulding machine is running, stopped, or in another configured operating state.
Production managers can use this information to identify interruptions and understand which machines need attention.
A centralised dashboard can display the status of multiple machines, helping supervisors monitor the production floor without relying entirely on manual updates.
2. Automated Production Counting
Accurate production counting is essential for calculating performance and comparing actual output with production targets.
Depending on available machine signals, the monitoring system can capture production cycles or component counts automatically.
For multi-cavity moulds, the counting configuration should account for the number of cavities and any cavities that are inactive or producing rejected parts.
Automated counting can reduce manual recording errors and provide more consistent production information.
Internal link opportunity: Link the anchor text Production Counter to the relevant Robato Systems product page in this section.
3. Cycle-Time Monitoring
Cycle-time monitoring helps compare actual machine cycles with the expected production cycle.
This is particularly useful in injection moulding, where small increases in cycle time can accumulate into significant output losses over a full shift.
Production teams can investigate whether slower cycles are related to cooling requirements, process adjustments, mould conditions, material changes, or machine performance.
4. Downtime Tracking and Reason Analysis
Downtime tracking helps identify when machines stop and how long interruptions last.
Manufacturers can configure downtime categories based on their production processes.
Examples include:
Machine breakdown
Mould changeover
Material shortage
Tooling or mould maintenance
Process parameter adjustment
Quality inspection
Operator-related delays
Planned maintenance
A structured reason-code system makes it easier to identify recurring problems and prioritise corrective actions.
5. OEE Dashboard for Multiple Machines
A centralised OEE dashboard can display machine-level and production-level performance information.
Depending on the software configuration, managers may review:
Availability percentage
Performance percentage
Quality percentage
Overall OEE
Total production count
Good and rejected components
Downtime duration
Production target achievement
This helps managers compare machine performance and identify production constraints across the facility.
6. Shift-Wise Production Reports
Production performance can differ between shifts due to machine setup, product mix, operator practices, maintenance activities, and production schedules.
Shift-wise reports help managers review output, downtime, and OEE for each defined shift.
These reports can also support discussions between production supervisors and maintenance teams about recurring problems.
7. Historical Production Analytics
Historical data helps manufacturers understand whether production performance is improving or declining over time.
Managers can analyse trends across machines, shifts, products, and production periods.
This supports better decisions about maintenance planning, process improvements, machine allocation, and production scheduling.
How OEE Monitoring Improves Injection Moulding Efficiency
OEE monitoring creates value when production teams use the information to identify losses and implement measurable improvements.
Reduce Unplanned Downtime
Machine stoppages directly reduce available production time.
By reviewing downtime frequency, duration, and reason categories, managers can identify recurring interruptions and prioritise the most significant problems.
For example, if a machine repeatedly stops because of a specific fault, the maintenance team can investigate the underlying cause instead of treating every incident as an isolated event.
Improve Cycle-Time Performance
Comparing actual cycle times with approved reference values helps identify production slowdowns.
If a machine consistently takes longer than expected to complete a cycle, the production team can investigate process settings, cooling time, material behaviour, mould conditions, and other relevant factors.
Any process adjustments should be validated against product quality, safety, and equipment specifications.
Increase Machine Utilisation
Machine utilisation improves when avoidable waiting time and production interruptions are reduced.
OEE data can help managers identify machines that spend significant time waiting for materials, mould changes, maintenance, or production instructions.
This information can support better coordination between production planning, stores, maintenance, and shop-floor teams.
Improve Quality Visibility
When rejected components are recorded alongside total output, managers can identify how quality losses affect machine effectiveness.
Quality trends may reveal recurring issues associated with specific moulds, materials, production jobs, or operating conditions.
This helps quality and production teams investigate problems using measurable information.
Support Better Production Planning
Reliable production data gives planners a more realistic understanding of machine capacity.
Actual cycle times, downtime trends, and historical output can help estimate production completion times and allocate jobs more effectively.
This is particularly useful in facilities that operate multiple machines and manufacture a variety of components.
Implementing OEE Monitoring in an Injection Moulding Factory
Successful implementation starts with understanding the existing machines, production processes, and data requirements.
A monitoring system should be configured around the actual operating conditions of the factory.
Step 1: Evaluate Existing Injection Moulding Machines
Begin by identifying the machines that need monitoring.
Record details such as:
Machine identification and location
Machine manufacturer and model
Controller type
Available communication interfaces
Existing production signals
Machine status indicators
Production counting requirements
This assessment helps determine the most appropriate data-collection approach.
Step 2: Define the OEE Calculation Rules
Before collecting data, define how OEE will be calculated.
Clarify:
Planned production time
Shift schedules
Planned stoppages
Ideal cycle times
Number of mould cavities
Total production count
Good and rejected component counts
Downtime categories
These definitions should be consistent across the machines being compared.
Step 3: Connect Machines to the Monitoring System
Machine data can be collected through supported controller interfaces, PLC signals, or suitable external sensors.
For machines with available communication interfaces, controller data may provide useful information such as machine status, cycle events, and alarms.
For older machines, selected signals may need to be collected through an external monitoring arrangement.
The integration method should be selected after checking signal availability, compatibility, and machine requirements.
Step 4: Configure Dashboards and Reports
Once the required data is available, configure dashboards that reflect the needs of operators, supervisors, production managers, and plant leadership.
Operators may need simple machine-status and production information, while managers may need comparative OEE reports and historical analysis.
Reports should make it easy to identify problems and take action rather than simply display large amounts of data.
Step 5: Train Production Teams
Operators and supervisors should understand how machine states are recorded, how downtime reasons are selected, and how production and quality information is interpreted.
Training helps create consistent data and improves adoption across shifts.
Step 6: Review Performance and Expand
Start with a pilot machine or production cell.
Validate machine signals, production counts, cycle-time calculations, downtime records, and OEE results.
Once the monitoring process is reliable, expand it to additional machines and production areas.
Common Challenges in Injection Moulding OEE Implementation
Even a capable monitoring system can produce misleading results if the underlying production data is not configured correctly.
Incorrect Cavity Configuration
Injection moulding machines often use multi-cavity moulds.
If the software assumes the wrong cavity count, expected production output and performance calculations may be inaccurate.
The configuration should reflect the actual number of active cavities for each production job.
Changing Cycle Times Across Products
Different components may require different cycle times because of mould design, material characteristics, component thickness, and cooling requirements.
Using one ideal cycle time for every production job can distort performance calculations.
Maintain approved reference cycle times by relevant machine, mould, and product combination.
Inconsistent Quality Recording
If rejected components are not recorded accurately, the quality percentage may appear better or worse than actual production conditions.
Define a consistent method for recording total components, good components, rejected components, and rework.
Poor Downtime Classification
If every machine interruption is recorded under a general downtime category, the reports will provide limited information about the underlying causes.
Create practical downtime categories and ensure that operators understand how to use them.
Ignoring Process Differences
Two injection moulding machines may have different capacities, mould configurations, and production requirements.
Comparing their OEE percentages without considering these differences can lead to incorrect conclusions.
Use OEE as a tool for understanding machine effectiveness within the context of each production process.
How to Choose the Right Injection Moulding OEE Software
Selecting the right software requires evaluating both technical compatibility and production requirements.
Consider the following factors before implementation.
Machine connectivity: Check whether the solution supports the communication interfaces and signals available on your injection moulding machines.
Production counting accuracy: Confirm that the system can handle cycle counting, multi-cavity moulds, and the required production units.
Cycle-time monitoring: Ensure that actual cycle times can be compared with appropriate reference values.
Downtime analysis: Check whether stoppages can be recorded, categorised, and analysed.
Quality tracking: Determine how the system handles good parts, rejected parts, and rework.
Dashboard visibility: Evaluate whether managers can monitor individual machines and the overall production floor from a centralised dashboard.
Reporting capabilities: Check whether the system supports shift-wise, machine-wise, and historical production reports.
Scalability: Consider whether the solution can expand as more machines or production facilities are added.
Integration requirements: Evaluate the need to connect with ERP, MES, PLCs, quality systems, or other manufacturing applications.
Implementation support: Review the availability of technical assistance, commissioning, training, and ongoing support.
A solution should fit the factory's actual production environment and provide reliable information that teams can use to improve operations.
Measuring the ROI of Injection Moulding OEE Software
The financial value of OEE monitoring depends on the production improvements achieved after implementation.
Potential benefits may include:
Reduced avoidable machine downtime
Increased production output
Better utilisation of existing machines
Lower quality-related production losses
Improved production planning
Better visibility into recurring process issues
For example, suppose an injection moulding machine operates for 420 planned production minutes per shift. Through downtime analysis, the production team identifies an opportunity to recover 20 minutes of avoidable stoppage time.
If the machine can use that recovered time to produce additional good-quality components, the manufacturer can estimate the potential value based on the contribution margin of those components.
However, recovered machine time does not automatically translate into additional revenue. Material availability, order demand, downstream capacity, staffing, and quality requirements must also be considered.
A practical ROI assessment should compare the cost of software, hardware, integration, training, and maintenance against the measurable benefits achieved over an agreed period.
Building a Continuous Improvement Process With OEE Data
OEE monitoring should be part of a continuous improvement process rather than a reporting activity that ends with a dashboard.
Injection moulding manufacturers can follow a simple improvement cycle:
Measure: Collect reliable machine, cycle-time, production, downtime, and quality data.
Analyse: Identify the largest production losses and investigate their root causes.
Improve: Implement targeted changes in maintenance, mould management, process settings, scheduling, or production procedures.
Verify: Compare performance before and after the changes to determine whether the improvements are sustained.
Regular reviews help production managers focus on measurable issues and ensure that corrective actions are followed through.
Over time, this approach can support more consistent production, improved machine utilisation, and better operational decision-making.
Conclusion
Injection moulding manufacturers need accurate visibility into how their machines perform throughout production. Production counts alone cannot explain why output falls below expectations or where valuable production time is being lost.
Injection Moulding OEE Software helps manufacturers monitor availability, performance, and quality while providing a structured way to analyse machine downtime, cycle-time losses, and production efficiency.
With reliable machine data, consistent OEE calculations, and regular performance reviews, production managers can identify improvement opportunities and make more informed decisions across the manufacturing floor.
Robato Systems helps manufacturers improve production visibility through machine monitoring and production data solutions. Explore the relevant monitoring capabilities to understand how they can support your injection moulding operations.
Want better visibility into your injection moulding production? Request a demo to discuss your machine monitoring and OEE requirements.